PLIERS PRODUCTION LINE

Pliers Manufacturing Process: Machines for Every Step

We supply the machines for every step of the pliers manufacturing process, from coining the forged blank to molding the handle. Forging and heat treatment of the blank are done upstream, before the first station. The line is built around 6–8 inch pliers and covers 5–12 inch with fixture and tool changes.

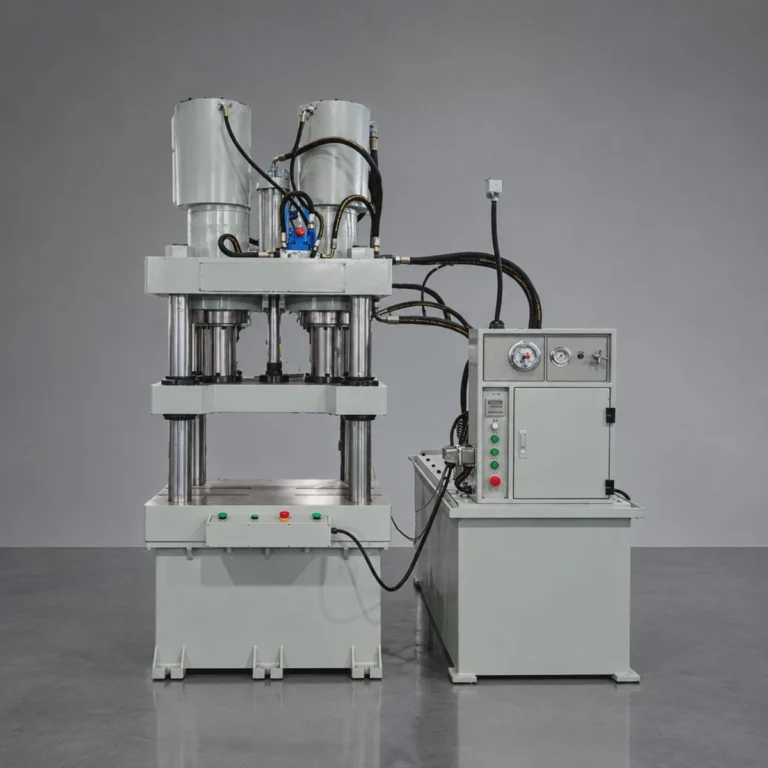
Pliers coining process

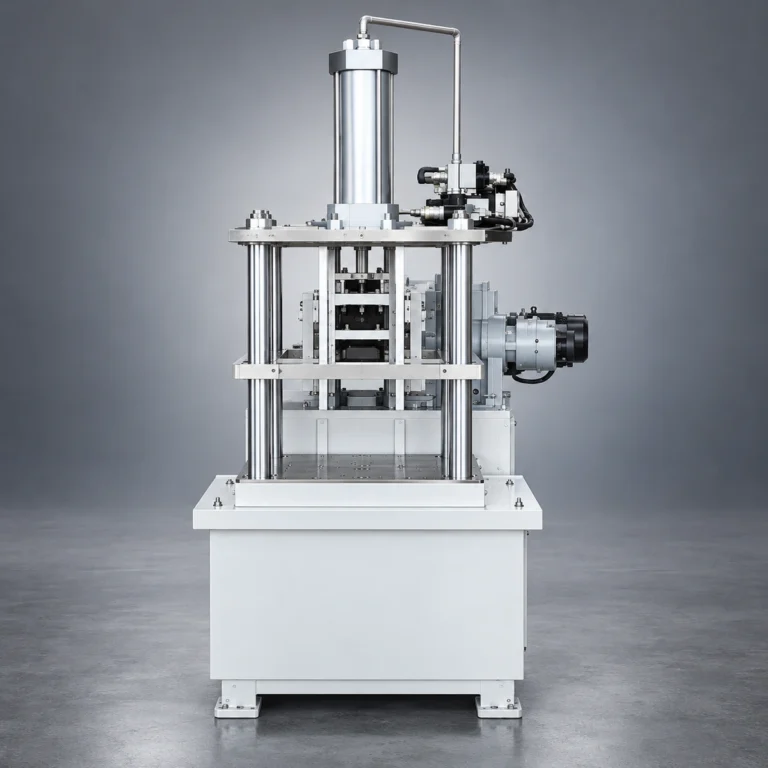
Hydraulic Coining Presses

Coining is the first station after forging. A hydraulic press squeezes the forged blank between dies to true its outline, emboss the lettering and level the jaws, so later stations start from a consistent part. The same press also punches and extrudes.

2500 kN force — fast, energy-saving and quiet

01
Pliers drilling and reaming process

Drilling & Reaming Machines

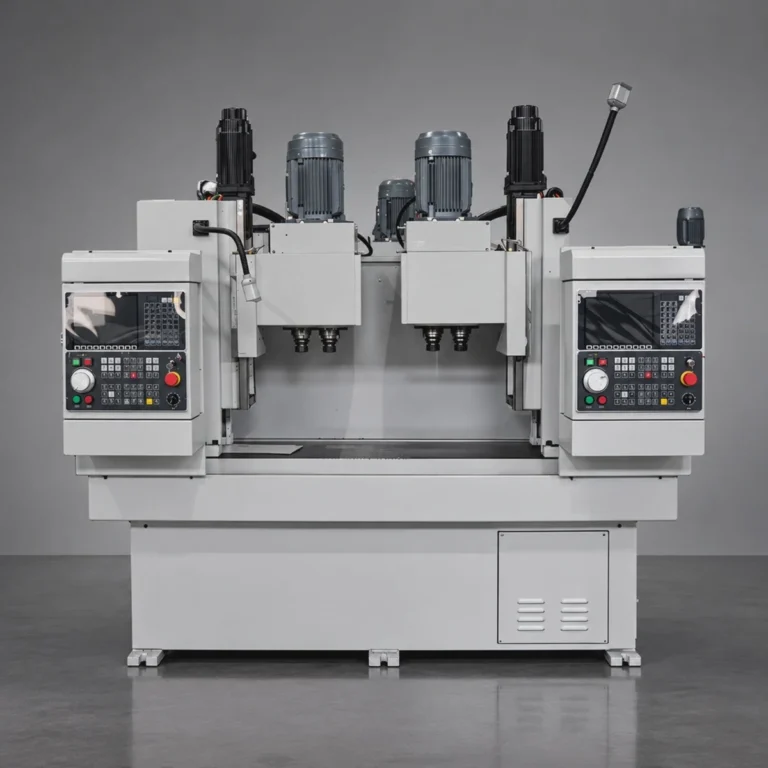
Drilling and reaming open the pivot hole on each pliers half, where the two halves are later riveted together, so its position decides how well the jaws line up. A four-axis twin-station machine drills and reams in high volume with light cuts, with servo-driven spindle box feed.

Pivot hole position within ±0.05 mm

02
Pliers drilling and countersinking process

Drilling & Countersinking Machines

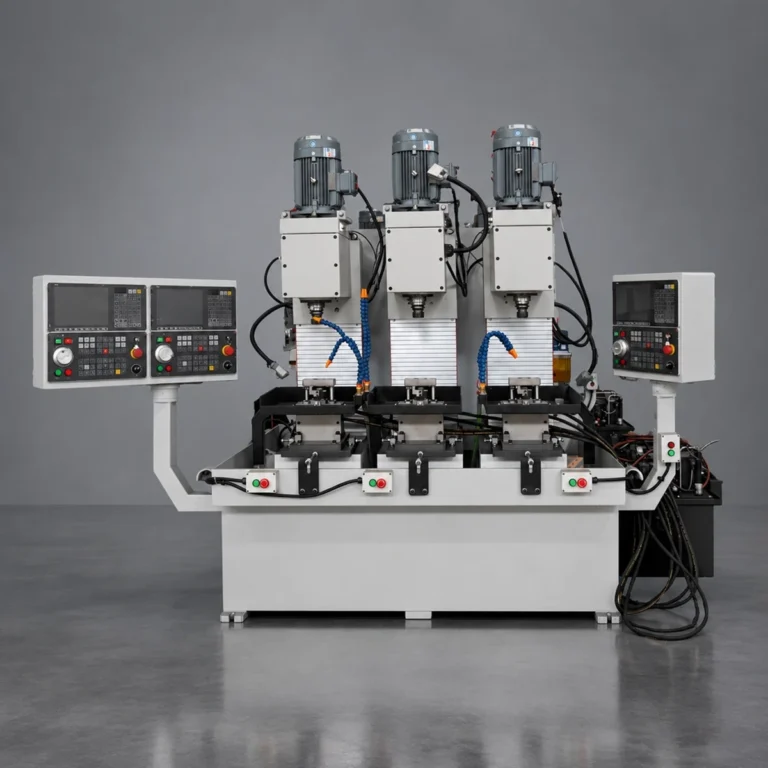
Countersinking cuts a chamfered seat at the pivot hole so the rivet head sits flush with the pliers surface. A three-axis CNC machine drills and countersinks in high volume with light cuts, with a servo-driven spindle box and variable-frequency spindle speed.

300 mm spindle box travel — servo rapid traverse

03
Pliers profile milling process

Profile Milling Machines

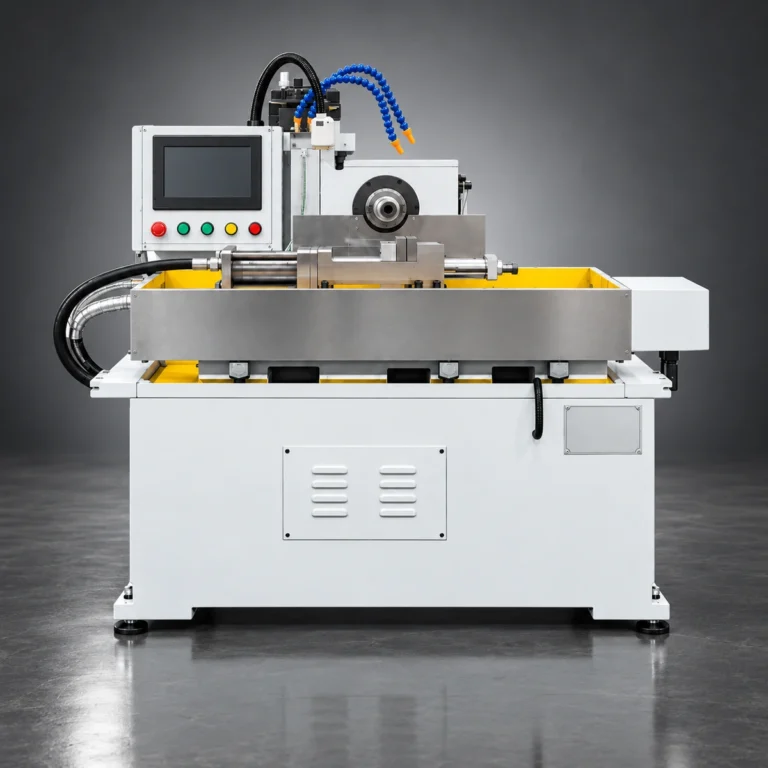
Profile milling rough-mills the outline of the coined blank and sets the shape that edge milling and grinding later finish. The horizontal machine suits combination and needle-nose pliers, with hydraulic table feed and clamping, infinitely adjustable feed and a smooth change from rapid to feed.

450 mm cross slide travel — foot-operated fixture

04
Pliers cutting edge milling process

Cutting Edge Milling Machines

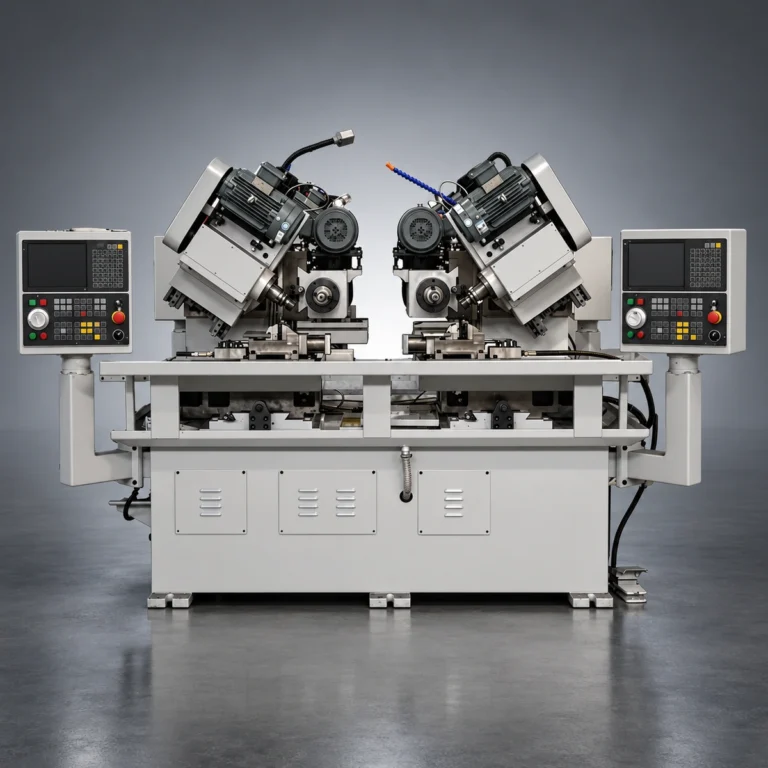
Cutting edge milling forms the inner and outer cutting edges and the gripping recesses of the pliers head. Both halves are clamped in one setup, so the two edges are milled to match and the jaws close cleanly. High-speed alloy cutters leave a good surface finish.

Both halves in one setup — twin-station CNC

05
Pliers stamping and notching process

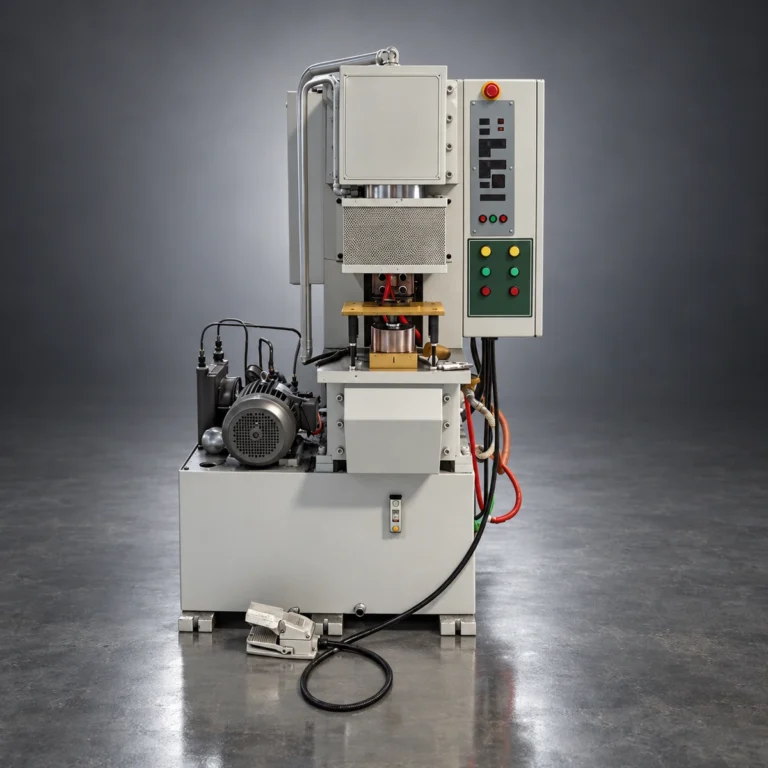
Stamping & Notching Presses

Stamping and notching press the markings and notches into the pliers body. A hydraulic press gives precise, repeatable pressure, so the markings come out clear and every notch has the same size from part to part. Operation is stable and simple.

200 kN rated force — 200 mm working stroke

06
Pliers hot riveting process

Hot Riveting Machines

Hot riveting heats the pivot rivet and sets it to join the two pliers halves. Riveting hot preserves the carbon structure of the material and gives a more secure joint. Closed-loop current control holds the current steady as supply and load change.

Closed-loop current control — hydraulic riveting head

07
Pliers double-side grinding process

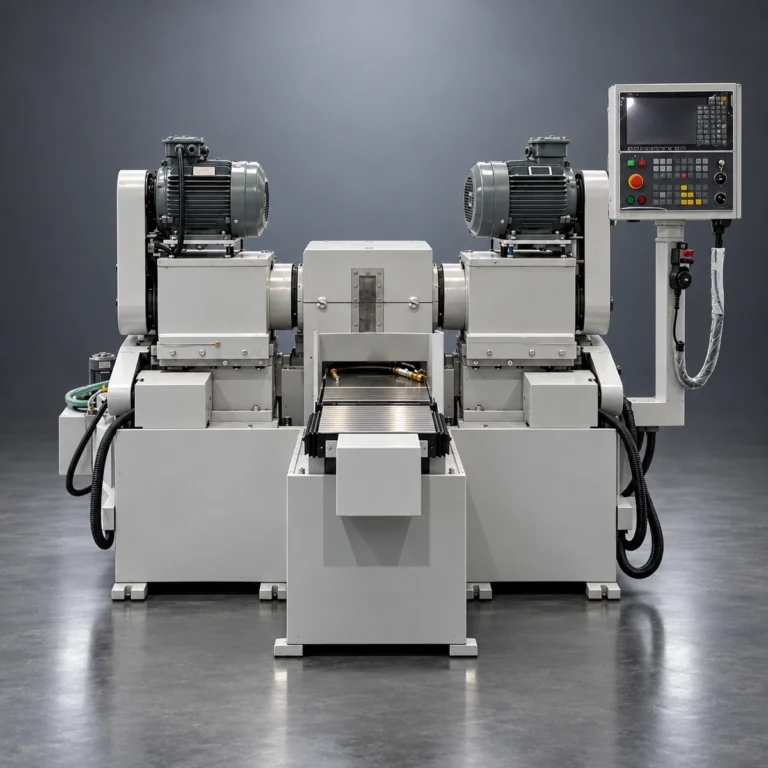
Double-Side Grinding Machines

Double-side grinding takes both faces of the pliers body to final thickness, so the two halves fit closely when assembled. Servo motors drive the table and both grinding heads, and one setup can grind two sets of parts to different thicknesses. It also grinds wrenches and chisels.

Body thickness within ±0.05 mm — auto wheel dressing

08
Pliers cutting edge laser hardening process

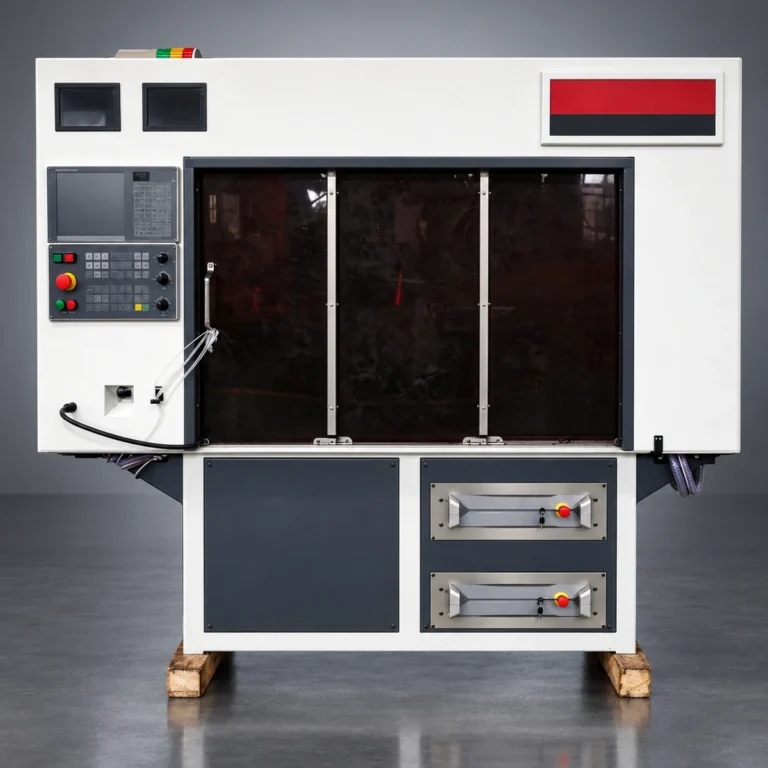
Cutting Edge Laser Hardening Machines

Laser hardening heats only the cutting edge instead of quenching the whole tool, so the line needs no quench oil and makes no waste water. Two laser heads harden both sides of the edge at once on combination, long-nose and diagonal pliers and bolt cutters.

25% less energy than conventional heat treatment

09
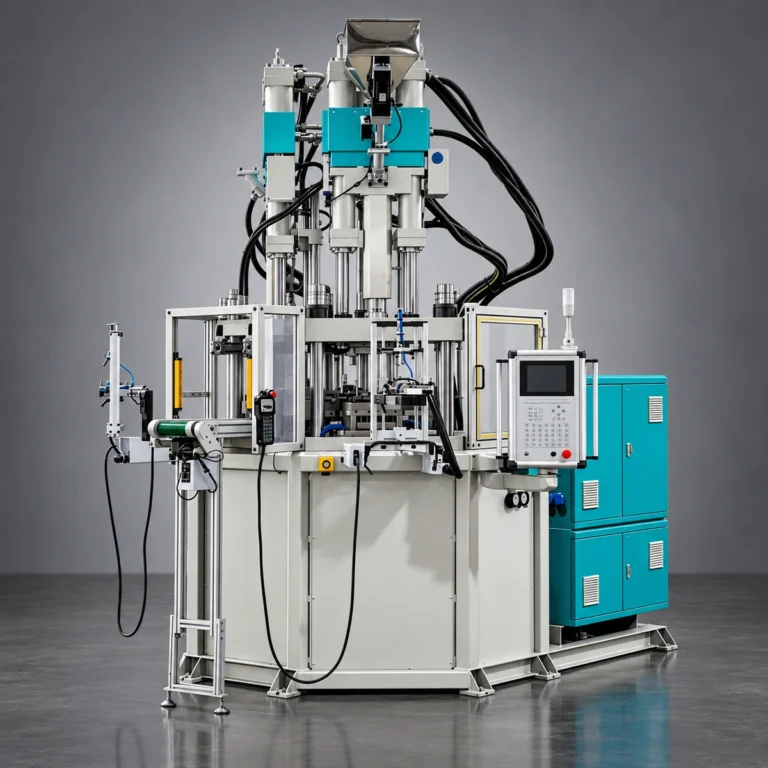
Pliers handle injection molding process

Handle Injection Molding Machines

Handle injection molding forms the insulated plastic handles, including two-color handles, as the last step of the line. A vertical machine with a rotary table loads and molds in parallel. Each mold has its own clamping cylinder, and the table upgrades from 4 to 6 or 8 stations.

160 t clamping force — up to 8 stations

10

Planning a Pliers Manufacturing Process?

Tell us the pliers types, sizes and output you need, and we will recommend single stations or a full line. Programs are preset, so operators only load, unload and monitor, and new staff learn the machines in 1–2 days. The machines run at an MTBF of at least 2,000 hours.

Scroll to Top

Get In Touch With Us!